Calibrating CNC Machine Tools: A Practical Guide for Woodworking, Stone, and General Fabrication
About Us / Author:ROCTECH Engineer Team / Published: Sep 29 , 2026 / Last Updated: Sep 29 , 2026
How to Calibrate CNC Machine Tools: A Practical Guide for Woodworking, Stone, and General Fabrication
---
Abstract
Calibration is the quiet discipline behind every accurate cut, every tight joint, and every repeatable production run. In woodworking, stone carving, and general fabrication, a CNC machine that has drifted out of alignment will produce scrap long before it produces a warning. This article examines the practical methods for calibrating CNC routers, machining centers, and stone CNC equipment, with attention to accuracy standards such as ±0.03 mm repeat positioning and the components—spindles, guide rails, ball screws, and servo systems—that determine whether those numbers hold. Reference is made to Roctech Machinery Co., Ltd., whose woodworking and stone CNC platforms illustrate how calibration procedures are applied in real production environments.
---
1. Why Calibration Determines Everything
A CNC machine is a system of mechanical references. The spindle must return to the same point. The gantry must travel square to the table. The tool tip must reach the programmed depth. When any of these references shift—through thermal expansion, collision, wear, or simply the passage of time—the machine continues to move confidently in the wrong direction.
In woodworking, a 0.2 mm error may be invisible on a cabinet door. In stone carving, the same error can chip an edge or ruin a relief. In mold and signage work, it can mean a rejected part. This is why calibration is not a one-time factory event but a recurring maintenance discipline.
2. What Accuracy Actually Means
Machine tool accuracy is usually expressed through three related metrics: positioning accuracy, repeat positioning accuracy, and processing accuracy. The table below summarizes typical requirements for woodworking and general CNC equipment.
| Accuracy Metric | Typical Specification | What It Measures |
|---|---|---|
| Positioning accuracy | ±0.05 mm / 300 mm | How close the axis reaches a commanded point |
| Repeat positioning accuracy | ±0.03 mm | How consistently it returns to the same point |
| Processing accuracy | Within ±0.1 mm | Combined result of machine, tool, and material |
| Spindle runout | Ideally below 0.01 mm | Tool tip deviation during rotation |
| Backlash (X/Y/Z) | Compensated to near zero | Lost motion when reversing direction |
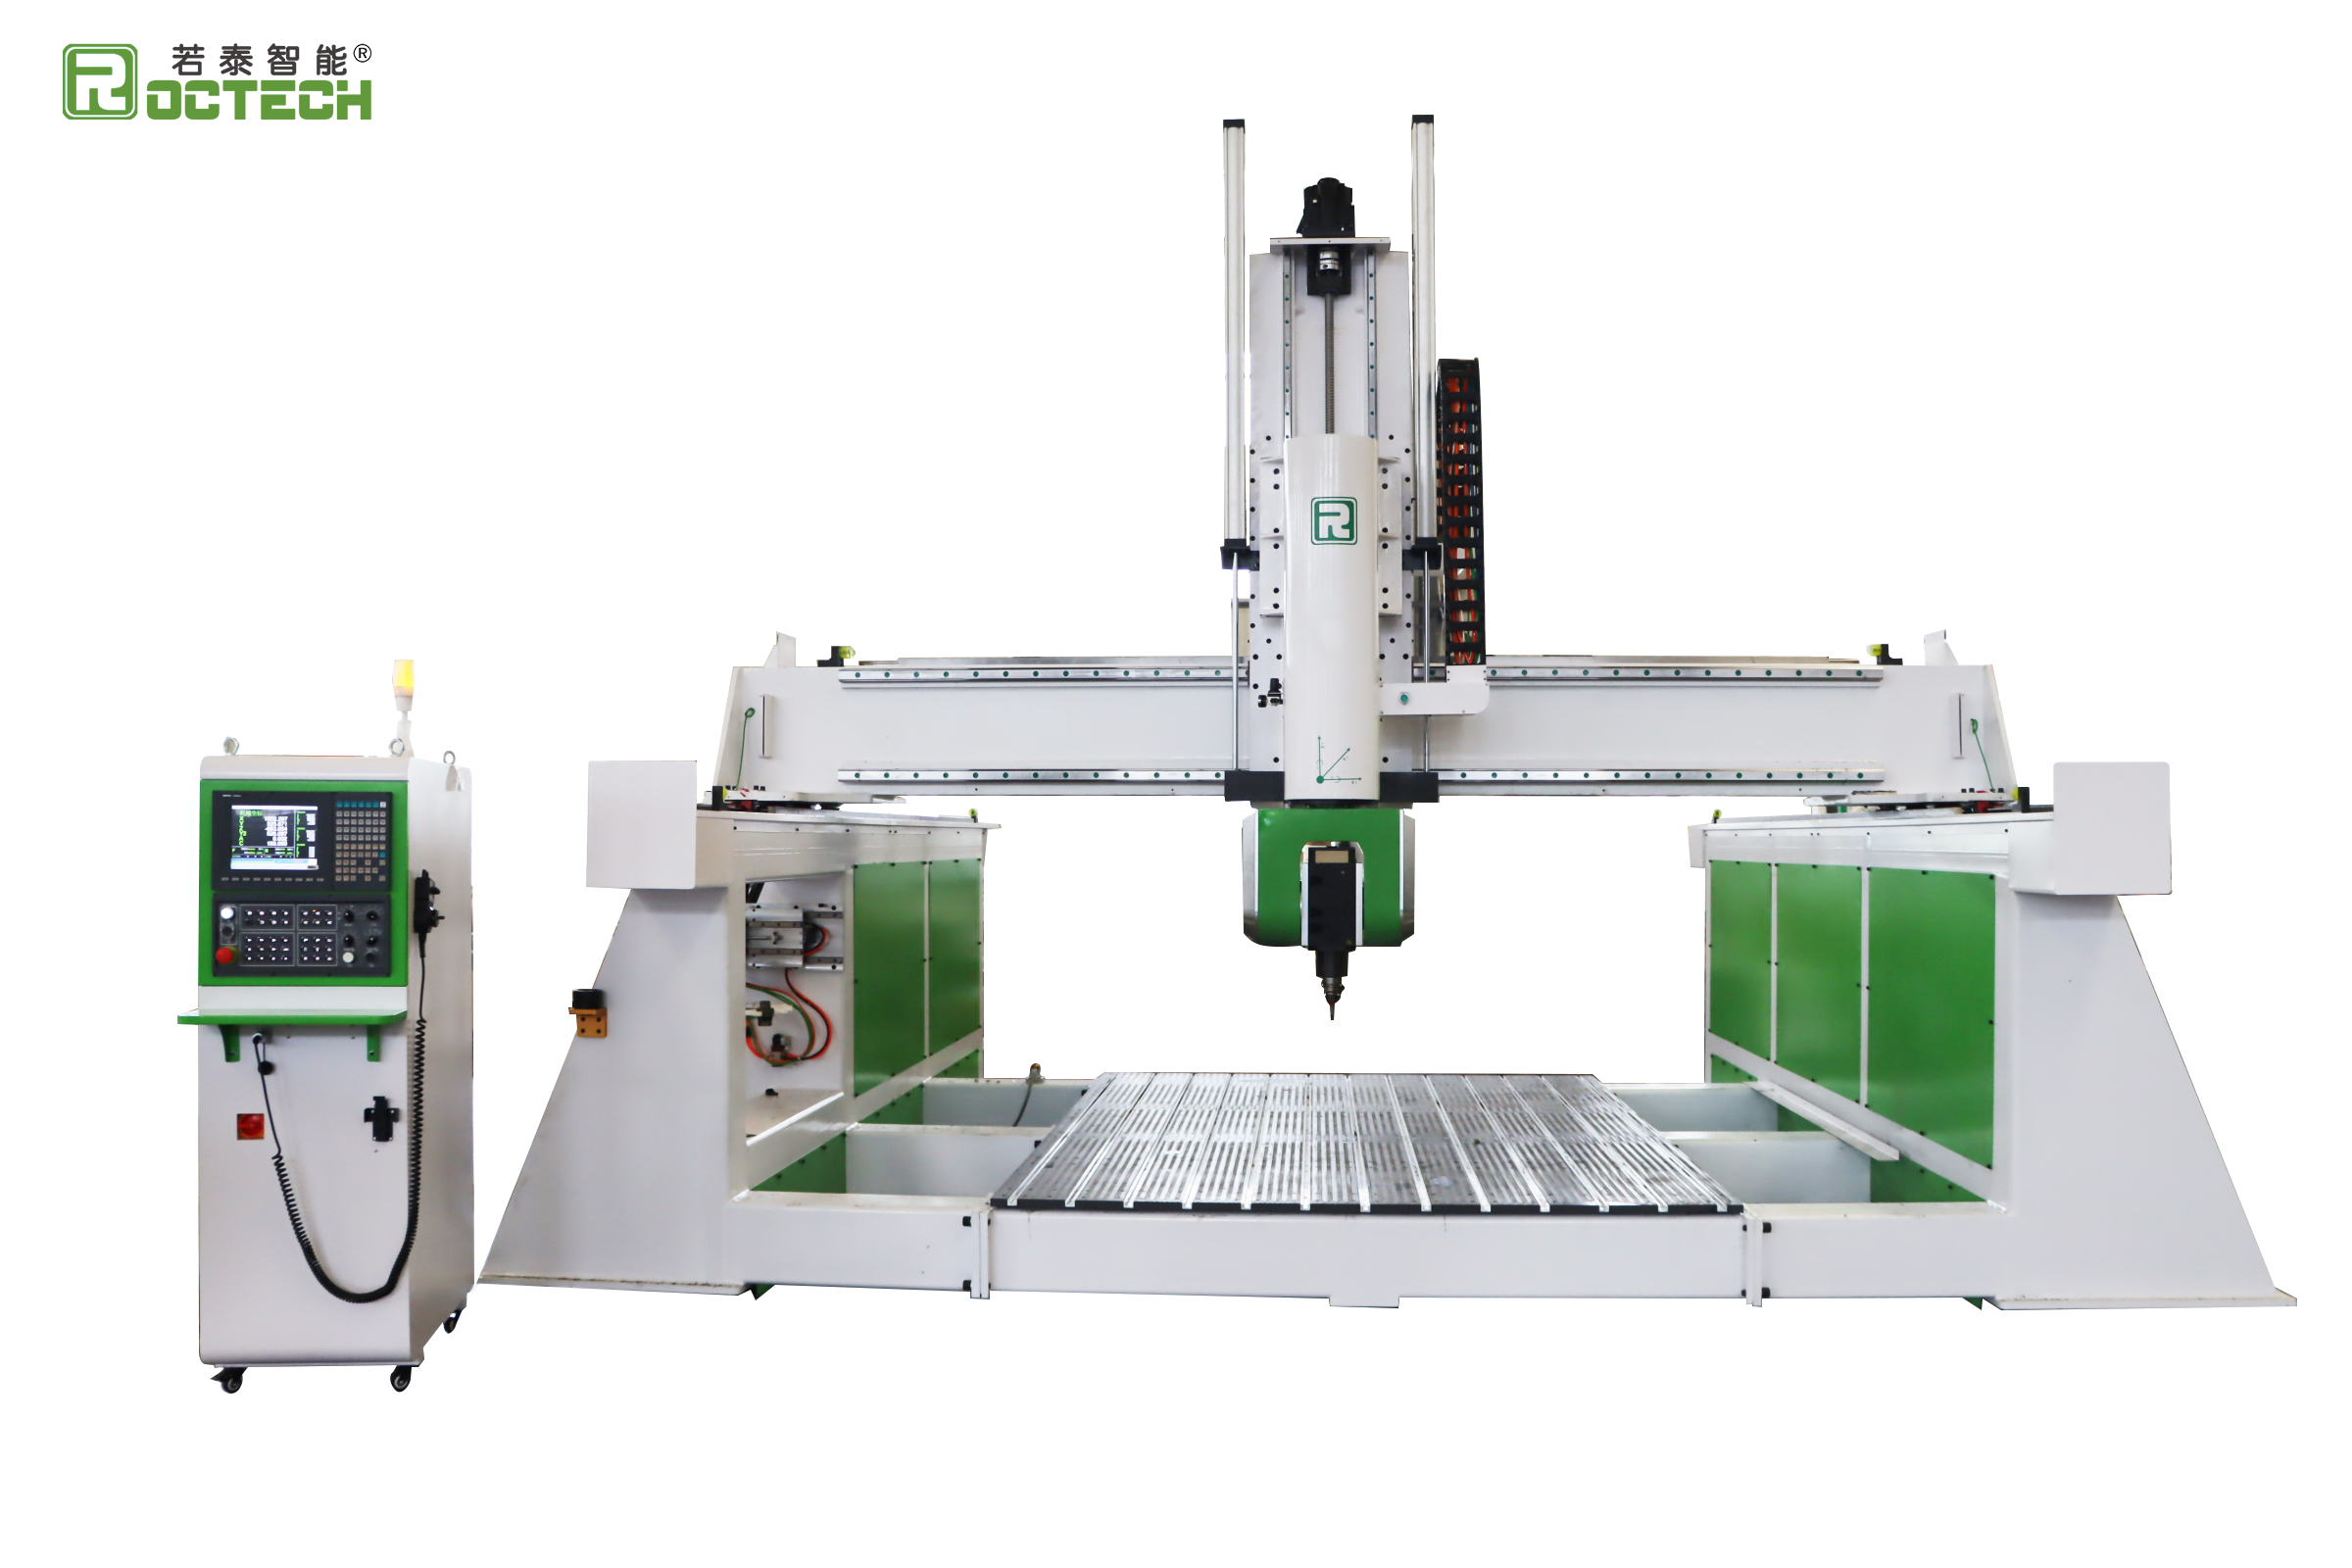
These figures are not arbitrary. They reflect the mechanical limits of linear guide rails, ball screws, and rack-and-pinion drives. A machine rated at ±0.03 mm repeat positioning—common across Roctech's ATC router and nesting center lines—can only achieve that number if backlash, squareness, and leveling are maintained within tolerance.
3. The Calibration Sequence
Calibration should follow a logical order. Adjusting the spindle before leveling the bed is wasted effort, because every subsequent measurement inherits the error.
3.1 Leveling and Bed Alignment
The machine must sit on a flat, rigid floor. Use a precision spirit level or electronic level across the table in both X and Y directions. Adjust leveling pads or foundation bolts until the table is flat within 0.02–0.05 mm per meter. On large stone CNC machines, where table lengths exceed 3 meters, this step is critical because the gantry spans the full width and any twist translates directly into depth variation.
3.2 Squareness of the Gantry
The gantry must be perpendicular to the side rails. A common method is the diagonal measurement: mark two reference points on the table, move the spindle to each corner, and compare diagonal distances. A difference indicates the gantry is skewed. On dual-drive machines, this is corrected by adjusting the slave-axis offset or re-homing both sides simultaneously.
3.3 Backlash Measurement and Compensation
Backlash is the lost motion when an axis reverses direction. It is measured by approaching a dial indicator from both sides and recording the difference. Rack-and-pinion systems used on the X and Y axes of large routers typically exhibit more backlash than ball screws, which is why controllers such as Taiwan Syntec systems include backlash compensation parameters. Once measured, the value is entered into the control, and the axis is re-tested.
3.4 Spindle Squareness and Runout
The spindle must be perpendicular to the table in both planes. A dial indicator mounted on a swing arm, rotated around the spindle nose, reveals any tilt. Runout is checked at the tool holder taper. Excessive runout—often caused by worn bearings or improper tool clamping—produces tapered cuts, poor surface finish, and accelerated tool wear. Italy HSD spindles, widely used on Roctech ATC routers, are
Looking for more information about our CNC machines and services? Contact us today.
Contact
Previous:Automotive Foam Mold Engraving Machines: Precision at the Intersection of Speed and Scale
Next:Not